From medical-grade tubing to industrial sealing, we provide durable rubber components tailored for regional operational demands.


Analyzing the intersection of high-temperature environments and silicone performance requirements.
Libya's industrial landscape, characterized by significant oil, gas, and emerging healthcare infrastructure, requires materials that can withstand extreme thermal fluctuations and corrosive environments. In such settings, standard rubber often fails, making Extruded Silicone Tube a critical component for fluid transport and sealing due to its superior thermal stability and chemical resistance.
The procurement shift in the region is moving toward high-compliance materials. As medical facilities upgrade, there is a growing demand for Medical-Grade Silicone Tube that meets international biocompatibility standards, ensuring safety in clinical applications while resisting the degradation typical of harsh regional climates.
For local engineers and procurement officers, this means prioritizing suppliers who hold comprehensive certifications like ISO 13485 and FDA. The ability to source precision-engineered components that balance flexibility with extreme durability is key to reducing maintenance cycles and operational downtime in Libyan facilities.
Tracing the transition from general-purpose rubber to specialized silicone applications.
Dependence on standard EPDM or Nitrile rubber for basic seals, often resulting in frequent replacements due to heat-induced cracking.
Integration of Food-Grade Silicone Tube and industrial seals to enhance hygiene and temperature resistance in processing plants.
Adoption of customized extrusion and liquid injection molding to meet strict medical and aerospace tolerances.
Increasing requirement for FDA and ISO certifications to ensure safety in food and medical supply chains within Libya.
Shift from off-the-shelf parts to tailored profiles, such as specialized Silicone Door Strip designs for energy-efficient climate control.
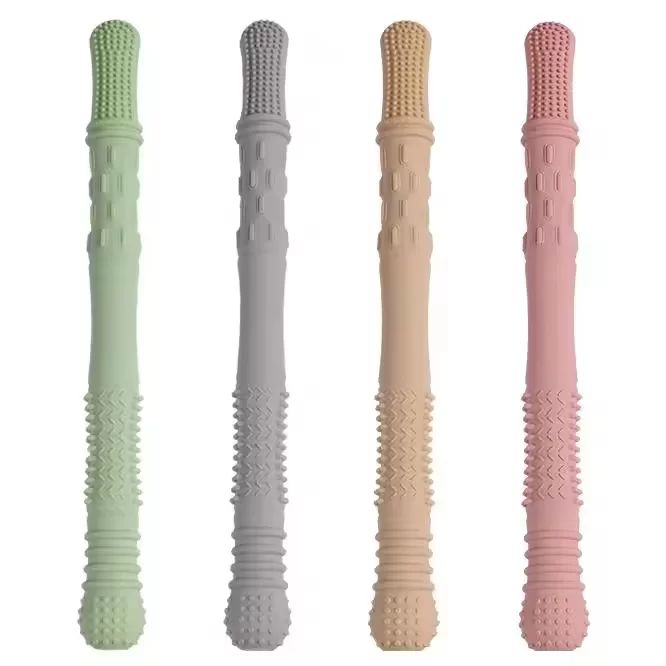
Growing demand for reusable and non-toxic alternatives, including the adoption of the Silicone Straw in hospitality sectors to reduce plastic waste.
Anticipating the needs of Libya's evolving industrial infrastructure.
Integration of advanced liquid injection molding to reduce waste and increase part consistency for medical devices.
Development of UV-resistant silicone compounds to prevent degradation in high-exposure outdoor environments.
Utilizing in-house mold development to accelerate the delivery of custom rubber components for urgent projects.
Aligning production with IATF 16949 and ISO 13485 to support the expansion of automotive and health sectors.
The future of material sourcing in Libya will likely prioritize vertical integration. Companies that can manage the process from R&D and mold design to final delivery offer a significant reduction in supply chain risk, which is vital for maintaining critical infrastructure.
Procurement managers should transition from evaluating suppliers based solely on price to assessing total lifecycle value. High-grade silicone, while having a different initial cost profile, reduces long-term expenditure through lower replacement rates and improved system reliability.
Practical use cases across various regional industries.
Implementing biocompatible tubing in Tripoli's clinics to ensure sterile fluid delivery, utilizing medical-grade silicone to prevent contamination and withstand sterilization cycles.
Deploying precision silicone door strips in cold storage warehouses to maintain internal temperatures against the extreme Libyan heat, reducing energy costs and food spoilage.
Integrating food-grade silicone tubes in beverage bottling plants to ensure compliance with hygiene standards and resist chemical cleaning agents.
Using high-temperature extruded silicone for protective sleeving and seals in monitoring equipment, preventing oil ingress and thermal failure in desert environments.
Replacing single-use plastics in high-end hotels with durable silicone straws, aligning commercial operations with global eco-friendly trends while maintaining luxury standards.
Our journey from a specialized manufacturer to a global solution provider.
Established as a dedicated player in the high-end silicone and rubber industry, focusing on precision manufacturing and material quality.
Expanded to four major production bases in Shenzhen, Huizhou, Dongguan, and Bangkok, covering over 170,000 square meters with a workforce of 1,000+ professionals.
Became a trusted supplier for global leaders like Samsung, Huawei, Sony, and Colgate, backed by certifications including FDA, ISO 13485, and IATF 16949.
Explore our full range of customized silicone applications and high-performance materials.
Answers to common technical and commercial queries from our clients.
Connect with our engineering team to discuss tailored rubber solutions for your projects in Africa - Libya. Let us help you enhance durability and compliance in your manufacturing process.
Discuss Your Requirements